Choosing the best Technical Ceramic manufacturer in China requires more than comparing prices or factory photographs. It demands evidence from production floors, testing rooms, and customer applications. Grand View Research estimates that the global advanced ceramics market will continue expanding through 2030, driven by electronics, medical devices, energy systems, and transportation. Its market analysis highlights alumina, zirconia, silicon carbide, and aluminum nitride as important material segments.
David W. Richerson, author of Modern Ceramic Engineering, states, “Ceramics are inorganic, nonmetallic materials.” The sentence is simple. The manufacturing challenge is not. A reliable supplier must control powder purity, molding pressure, sintering temperature, grinding accuracy, and final inspection. For example, a zirconia seal may look flawless while hiding internal porosity. That small defect can cause leakage after repeated thermal cycles.
The best Chinese manufacturer should therefore show measurable capability. Look for ISO 9001 systems, batch traceability, calibrated CMM equipment, material certificates, and documented dimensional results. Ask for data on density, flexural strength, dielectric loss, surface roughness, and process capability. Customer references from semiconductor, medical, or aerospace projects add valuable experience. So does a clear response to nonconforming parts.
A polished website proves little. A detailed inspection report proves more. Still, no ranking is perfect. Supplier performance can change with equipment, staff, or production volume. This article will compare leading Chinese manufacturers through technical evidence, application experience, quality controls, customization ability, and delivery reliability. The goal is practical judgment, not an easy winner.
Technical ceramics are engineered, inorganic, non-metallic materials made for demanding performance. ISO 20507 places fine ceramics within advanced technical applications, rather than ordinary tableware or structural clay products. Their scope includes alumina, zirconia, silicon carbide, silicon nitride, and ceramic matrix composites. These materials may resist heat, wear, corrosion, electrical leakage, or sudden temperature changes. The boundary is not perfectly clean. Some applications combine ceramic bodies with metal coatings, polymers, or conductive phases.
The market is expanding because equipment needs smaller, harder, and more stable components. MarketsandMarkets’ 2024 Advanced Ceramics Market report estimated a value of about 11.4 billion US dollars in 2024. It also projected growth to approximately 16.5 billion dollars by 2029. Such figures describe a broad market, not every Chinese factory. A capable manufacturer should therefore show material certificates, dimensional inspection records, firing data, and traceability for each batch.
Details matter. A valve seat may need a polished sealing surface within micrometre-level tolerance. An electrical insulator may require controlled dielectric strength after repeated heating cycles. Engineers should ask about shrinkage variation, porosity, thermal shock testing, and machining capacity. Production experience helps, but it can also create blind spots. A familiar formula may fail when the geometry changes. Supplier selection should compare verified test results with the actual service environment, not rely on catalogue claims or low unit prices.
Choosing a technical ceramic manufacturer in China requires more than comparing unit prices. The real test is process control, material knowledge, and production evidence. Start by checking whether the factory understands your ceramic grade and operating conditions. Alumina, zirconia, and silicon nitride each behave differently during forming and firing. Ask for shrinkage data, machining tolerances, and previous test methods. A capable engineering team should explain tradeoffs in plain language. That matters.
Request samples made with the same pressing, machining, and firing processes as your order. Inspect flatness, hole diameter, surface finish, and edge quality against your drawing. Do not accept a polished sample as proof of stable production. I have seen attractive prototypes fail after repeated thermal cycling. Production records deserve equal attention. Look for batch traceability, furnace logs, inspection reports, and corrective-action records. Check calibration certificates for measuring equipment. Independent testing can strengthen confidence, especially for demanding applications.
Reliable communication is another practical criterion. Can the team answer technical questions without avoiding details? Clear responses reveal experience; vague promises usually create expensive revisions. Review capacity, lead times, packaging, and quality responsibilities before signing. A documented quality system should support consistent output, not merely satisfy an audit. No evaluation is perfect. Small pilot orders still provide valuable evidence. Monitor dimensional results, delivery condition, and response speed during that stage. A factory may offer excellent engineering support yet struggle with volume, so capacity claims require careful verification.
| Evaluation Dimension | Key Data or Benchmark | Recommended Evidence to Request | Why It Matters | Priority |
|---|---|---|---|---|
| Material Selection | Confirm whether the proposed grade is alumina, zirconia, silicon carbide, silicon nitride, steatite, or another technical ceramic, with the exact composition and grade designation documented. | Material datasheet, chemical composition, grade specification, and application compatibility statement. | Different ceramics provide different combinations of wear resistance, toughness, thermal shock resistance, electrical insulation, and corrosion resistance. | High |
| Purity and Composition Control | High-purity alumina is commonly specified at 95%, 96%, 99%, or 99.5% Al2O3, depending on the application. The selected value should match the required electrical, wear, and thermal properties. | Batch certificate, chemical analysis, impurity limits, and sampling procedure. | Small variations in composition can affect density, dielectric performance, corrosion resistance, sintering behavior, and dimensional stability. | High |
| Bulk Density and Open Porosity | Dense technical ceramics generally require low open porosity. Typical dense alumina grades are often specified near 3.7–3.9 g/cm3, while zirconia is commonly near 5.8–6.1 g/cm3; actual values are grade-dependent. | Test report using an applicable density and porosity method, such as ASTM C20 or ISO 18754. | Density and porosity influence strength, fluid penetration, dielectric reliability, corrosion resistance, and service life. | High |
| Flexural Strength | Typical room-temperature strength varies widely: engineering alumina may be approximately 250–500 MPa, zirconia approximately 700–1,200 MPa, and silicon nitride approximately 600–1,000 MPa, depending on grade and test method. | Recent test reports, specimen geometry, test method, surface condition, and statistical distribution such as Weibull data. | Ceramics are brittle, so strength variation and surface defects can strongly affect component reliability. | High |
| Fracture Toughness | Representative ranges are often about 3–5 MPa·m1/2 for alumina, 5–10 MPa·m1/2 for zirconia, and 5–8 MPa·m1/2 for many silicon nitride grades. | KIC test data, test configuration, calculation method, and minimum guaranteed value. | Fracture toughness indicates resistance to crack growth and is important for impact, cyclic loading, and edge-sensitive components. | High |
| Hardness and Wear Resistance | Vickers hardness is commonly around 1,500–2,000 HV for alumina, approximately 1,100–1,600 HV for zirconia, and up to about 2,000–2,500 HV for many silicon carbide grades. | Hardness test report, indenter load, surface preparation, wear test results, and counterface material. | Hardness alone does not fully predict wear performance; actual wear testing should reflect the operating load, speed, lubrication, and environment. | High |
| Thermal Conductivity | Approximate room-temperature values may range from 20–35 W/m·K for alumina, 15–30 W/m·K for zirconia, and 80–180 W/m·K for silicon carbide, depending on purity and microstructure. | Thermal conductivity report, measurement temperature, test method, and material orientation if applicable. | Thermal conductivity affects heat dissipation, thermal gradients, component temperature, and thermal shock behavior. | High |
| Coefficient of Thermal Expansion | Typical average values are approximately 7–9 × 10⁻⁶/K for alumina, 9–11 × 10−6/K for zirconia, and 3–5 × 10⁻⁶/K for silicon carbide. | Thermal expansion curve, test temperature range, and applicable ISO or ASTM test method. | Matching thermal expansion with adjoining metals, glass, or ceramics helps prevent cracking and joint failure. | High |
| Maximum Service Temperature | Maximum temperature depends on atmosphere, mechanical load, thermal cycling, insulation requirements, and component geometry. A material datasheet limit should not be treated as a universal operating limit. | Temperature-rating documentation, thermal cycling data, atmosphere limitations, and application-specific validation. | Oxidation, creep, phase transformation, sealing materials, and thermal gradients may reduce performance below the nominal material limit. | High |
| Dimensional Tolerances | As-fired tolerances are generally wider than machined tolerances. Final tolerances should be stated on the drawing and separated into green, sintered, and post-machined conditions. | Capability study, inspection plan, calibrated measurement records, and sample dimensional report. | Controlled tolerances are essential for assemblies, sliding fits, seals, bearings, and components with strict alignment requirements. | High |
| Surface Finish | Ground or lapped technical ceramic surfaces can achieve significantly lower roughness than as-fired surfaces. The required Ra value should be specified according to sealing, friction, optical, or electrical needs. | Surface-roughness report, measurement equipment details, inspection locations, and representative samples. | Surface finish affects friction, leakage, wear, dielectric behavior, contact fatigue, and crack initiation risk. | Medium |
| Complex-Shape Manufacturing Capability | Evaluate the complete process chain: powder preparation, forming, debinding, sintering, grinding, lapping, drilling, metallization, and assembly. | Process flow chart, comparable non-branded samples, tooling plan, and documented process controls. | Technical ceramics shrink during sintering, and complex geometries can create distortion, warpage, or internal defects. | High |
| Quality Management System | A mature supplier should operate a documented quality system with controlled procedures, nonconformance management, corrective action, calibration, and internal audits. | Current quality-management certificate, audit summary, process-control plan, and corrective-action records with confidential information removed. | A quality system supports repeatability and reduces the risk of inconsistent batches and undocumented process changes. | High |
| Inspection and Test Equipment | Relevant equipment may include coordinate measuring machines, optical measurement systems, profilometers, density testers, hardness testers, microscopes, and strength-test fixtures. | Equipment list, calibration certificates, measurement uncertainty information, and inspection-frequency schedule. | Reliable measurements are necessary to verify dimensional, mechanical, thermal, and surface-quality requirements. | High |
| Traceability | Each production lot should be traceable to raw-material batch, forming process, sintering cycle, machining records, inspection results, and shipment documentation. | anonymized lot record, traveler, certificate of conformity, and retention-period policy. | Traceability enables root-cause analysis, controlled recalls, and reliable comparison between production lots. | High |
| Prototype and Sample Validation | Before mass production, samples should be evaluated against the approved drawing, material specification, functional requirements, and relevant environmental conditions. | First-article inspection report, dimensional results, functional test report, and sample approval procedure. | Prototype validation identifies shrinkage, machining, assembly, and performance issues before tooling and production quantities increase. | High |
| Production Capacity and Lead-Time Control | Assess monthly capacity, furnace capacity, machining capacity, tooling availability, normal lead time, and contingency planning rather than relying only on quoted delivery dates. | Capacity statement, production schedule example, bottleneck analysis, and escalation procedure for delayed orders. | Capacity transparency helps prevent delays when demand increases or when specialized sintering and precision-machining steps are required. | Medium |
| Packaging and Export Protection | Packaging should protect brittle parts from shock, vibration, moisture, contamination, and abrasion during domestic and international transport. | Packaging specification, drop or vibration test approach, labeling sample, and damage-claim process. | Even a correctly manufactured ceramic component can be damaged by inadequate separation, cushioning, or moisture protection. | Medium |
| Technical Communication | Drawings, tolerances, material requirements, test conditions, change approvals, and nonconformance decisions should be documented in clear written form. | Technical review checklist, engineering-change procedure, drawing-control process, and response-time expectations. | Clear communication reduces specification ambiguity and prevents unapproved substitutions or process changes. | High |
| Total Cost of Ownership | Compare material, tooling, machining, inspection, packaging, shipping, rejection risk, maintenance, and expected service life—not only the unit price. | Itemized quotation, tooling terms, warranty conditions, replacement-cost assumptions, and lifecycle comparison. | A lower initial price may result in higher total cost if it produces more defects, shorter service life, or greater downtime. | High |
| Application-Specific Testing | Validation should reproduce the actual load, temperature, chemical exposure, electrical conditions, pressure, cycling frequency, and installation method whenever possible. | Test protocol, acceptance criteria, test duration, failure analysis, and final validation report. | Generic datasheet values cannot fully predict performance under a specific operating environment. | High |
| Supplier Audit and Risk Review | Review process controls, subcontracting, raw-material sourcing, equipment maintenance, business continuity, cybersecurity, and change-management practices. | Audit checklist, risk register, subcontractor disclosure, business-continuity plan, and approved-change history. | Operational risks can affect supply continuity and product consistency even when the technical samples meet requirements. | Medium |
Note: Technical-property ranges are general reference values for common ceramic families. Actual performance depends on grade, purity, porosity, microstructure, processing route, test method, specimen geometry, and operating conditions. Final purchasing decisions should be based on an approved specification and application-specific validation.
Choosing the best technical ceramic manufacturer in China requires more than comparing catalog prices. Product categories reveal real expertise. Common materials include alumina, zirconia, silicon nitride, steatite, and cordierite. Each serves different conditions. Alumina suits electrical insulation and wear parts. Zirconia supports tougher cutting and medical components. Silicon nitride handles heat, friction, and demanding mechanical loads.
Manufacturing capability matters equally. Reliable facilities combine dry pressing, isostatic pressing, injection molding, extrusion, and tape casting. Complex parts may require diamond grinding or precision CNC machining after sintering. A strong supplier should control shrinkage, surface finish, flatness, and dimensional tolerance through documented inspection. Ask for material data, process records, sample testing, and traceability. Small details matter.
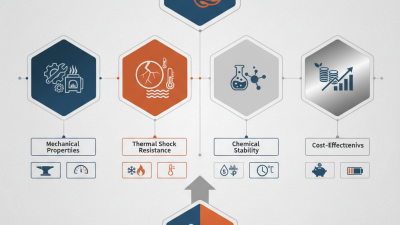
Real production is rarely perfect. No supplier gets every geometry right on the first trial. I have seen drawings pass review but fail during firing because of uneven wall thickness. That lesson is easy to overlook. Experienced manufacturers discuss draft angles, machining allowance, kiln loading, and expected deformation before production begins. Their laboratories should test density, hardness, dielectric strength, thermal shock resistance, and chemical stability. They should also explain limitations clearly, rather than promise every performance target. A capable Chinese manufacturer is not simply a ceramic parts vendor. It is a process partner that can turn material selection into stable, repeatable production.
The best technical ceramic manufacturer in China should prove quality through systems, not polished claims. ISO’s 2022 Survey recorded more than 1.2 million ISO 9001 certificates worldwide. This scale shows certification matters, but it does not guarantee excellent ceramic parts. Buyers should request valid certificates, audit scope, and recent surveillance records. ISO 14001 supports environmental control, while ISO/IEC 17025 accreditation strengthens laboratory test reliability.
Look for traceable powder batches, calibrated furnaces, and documented sintering curves. A serious supplier should report density, hardness, fracture toughness, dielectric strength, and dimensional variation. Testing should follow recognized methods, such as ASTM or ISO standards. Ask for inspection data from the actual production lot. Not a brochure sample. A 2024 advanced ceramics market report estimated global demand would grow at roughly 6–7% annually through 2029. That growth increases pressure on capacity, consistency, and technical support.
Research innovation also deserves practical evidence. Check whether engineers develop improved alumina, zirconia, silicon nitride, or ceramic composites for specific operating conditions. Examine pilot results, failure analysis, and peer-reviewed technical cooperation. Patents alone can mislead. I would still question any supplier showing perfect results without variation. Real production includes occasional defects, and reliable manufacturers explain their corrective actions clearly. Their research team should connect material science with machining, thermal cycling, and customer validation.
Choosing the best technical ceramic manufacturer in China starts with your application, not a polished website. Define temperature, electrical insulation, wear, chemical exposure, dimensions, and expected service life. Alumina, zirconia, silicon nitride, and other ceramics behave differently under stress. Small differences matter. A manufacturer should recommend a material based on measured conditions, not simply promote its most common product.
Ask for material data, dimensional tolerances, surface-finish limits, and inspection records. Check whether the factory can produce your required shape, especially thin walls, holes, or complex curves. Request sample parts before approving mass production. Test them under realistic heat, pressure, vibration, or chemical contact. An experienced engineering team should explain failures clearly and suggest practical design changes. Vague promises are warning signs.
During supplier evaluation, review process controls, raw-material traceability, kiln records, and final inspection methods. A quality system such as ISO 9001 can support reliability, but certification alone proves little. Speak with the production and quality teams, not only a salesperson. If possible, arrange a factory audit and compare actual equipment with the quoted process. However, a remote audit may not reveal every weakness. Keep that limitation visible. Lead time, packaging, export documents, and after-sales communication also affect your application. A low quotation can become expensive when tolerances drift or replacement parts arrive late. Include these risks in your decision.